20T/H Containerized Reverse Osmosis Water Purification System Shipped to South Africa
We are pleased to share this project update: Our 20T/H containerized RO water purification system has finished production, assembly and full-load testing, ready for shipment to South Africa. The complete water treatment unit is pre-installed inside a standard shipping container, designed for fast deployment and anti-corrosion performance to adapt to South Africa’s local climate and borehole water conditions.

Equipped with complete multi-stage pretreatment system and high-efficiency reverse osmosis membrane components, the equipment can effectively filter sediment, rust, heavy metals and other impurities in local well water. The system can stably produce 20 tons of purified water per hour. With fully automatic intelligent PLC control, the system supports long-time continuous operation, featuring simple operation and low daily maintenance cost.
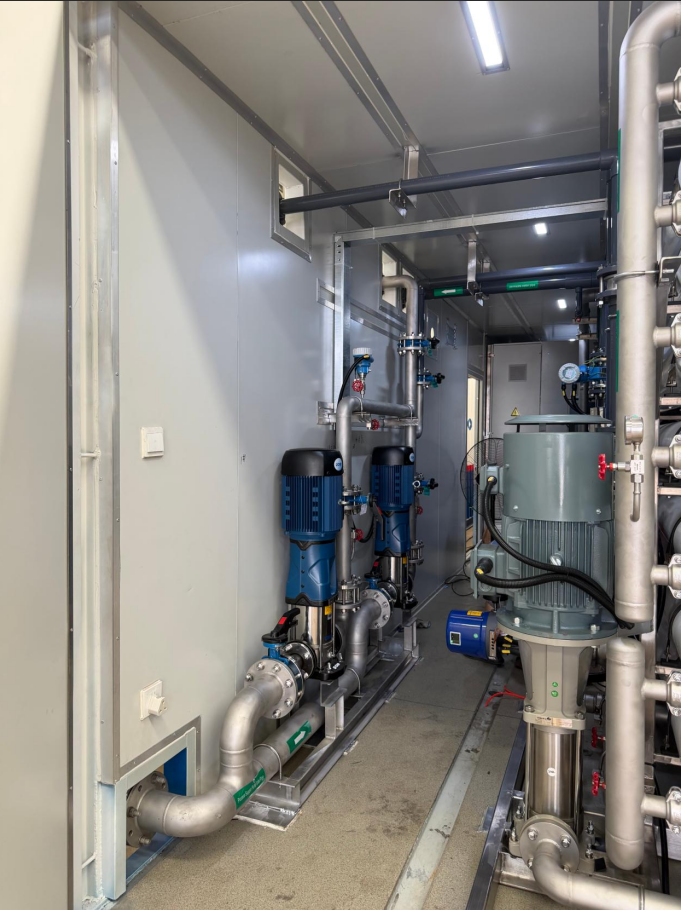
The containerized design saves on-site construction work. After delivery, customers only need to connect water inlet, outlet and power supply to start running. It is ideal for mining sites, industrial parks, large communities and factory water supply projects in South Africa. Before packaging and delivery, the whole system undergoes strict continuous running test to guarantee stable performance after on-site commissioning. We provide English operation manuals, remote technical guidance and long-term spare parts supply to support local customers’ water treatment projects.
 Whatsapp Scan


